The shrink wrap on the second carton had split somewhere on the water. Inside, two trays of 22 mm buttons sat loose, one of them upside down with the contact blocks separated from the heads and rolling around the tray like loose change. The driver wanted a signature. At the receiving end, a panel builder had a production slot booked for the next morning. Ten minutes at the tail lift would decide whether that slot held.
This piece is about that ten minutes: what a buyer or storekeeper can actually check on a push button shipment at the dock, without a lab, and what each finding usually means. It covers modular 22 mm and 16 mm industrial push buttons of the IEC 60947-5-1 type. One disclosure first: ACXION packs and ships the ranges used as examples, so this is the outgoing QC view from our own loading bay, written for the receiving end.
Certificates describe the batch. The carton is what you get.
A CE declaration or a test report says the type passed. It says nothing about your carton. Did the trays shift? Did a seal take a knock? Did the picker grab the wrong contact block variant? Only the carton can answer those. Type approval is one question. Shipment quality is another. You can check the second in ten minutes with a pocket tool. The first, not at all.
Everything below uses kit you already own. A multimeter. The purchase order. Two minutes per sample. If the shipment is small, sample all of it. Got a pallet? Pull cartons from different layers. The top carton is always the least knocked about one.
The ten-minute routine
- Start at the bottom of the carton. That is where the weight sat and where the damage collects. If the bottom trays are intact, the top ones are almost always fine.
- Check the model code against the PO. The carton label lies more often than the part does, so read the code off the part itself. The XH2 and LA135 codes encode head style, contact arrangement and contact material, and one character of difference is a different part. Code tables sit in the catalogues on the page de téléchargements.
- Operate every sampled unit ten times. You are feeling for a crisp click and a full return, not measuring anything. A gritty or lazy return at this stage is a packing or assembly issue, and it shows up here for nothing.
- Ring out the contacts. Multimeter on continuity, probe the terminals, press. NO closes, NC opens, and on a 1NO1NC block both happen on the same press. Twenty seconds per unit.
- Look at the contact faces. Silver should look silver. Scratches through the plating, or a face that looks scorched on a brand new part, mean a production or storage problem worth a photo.
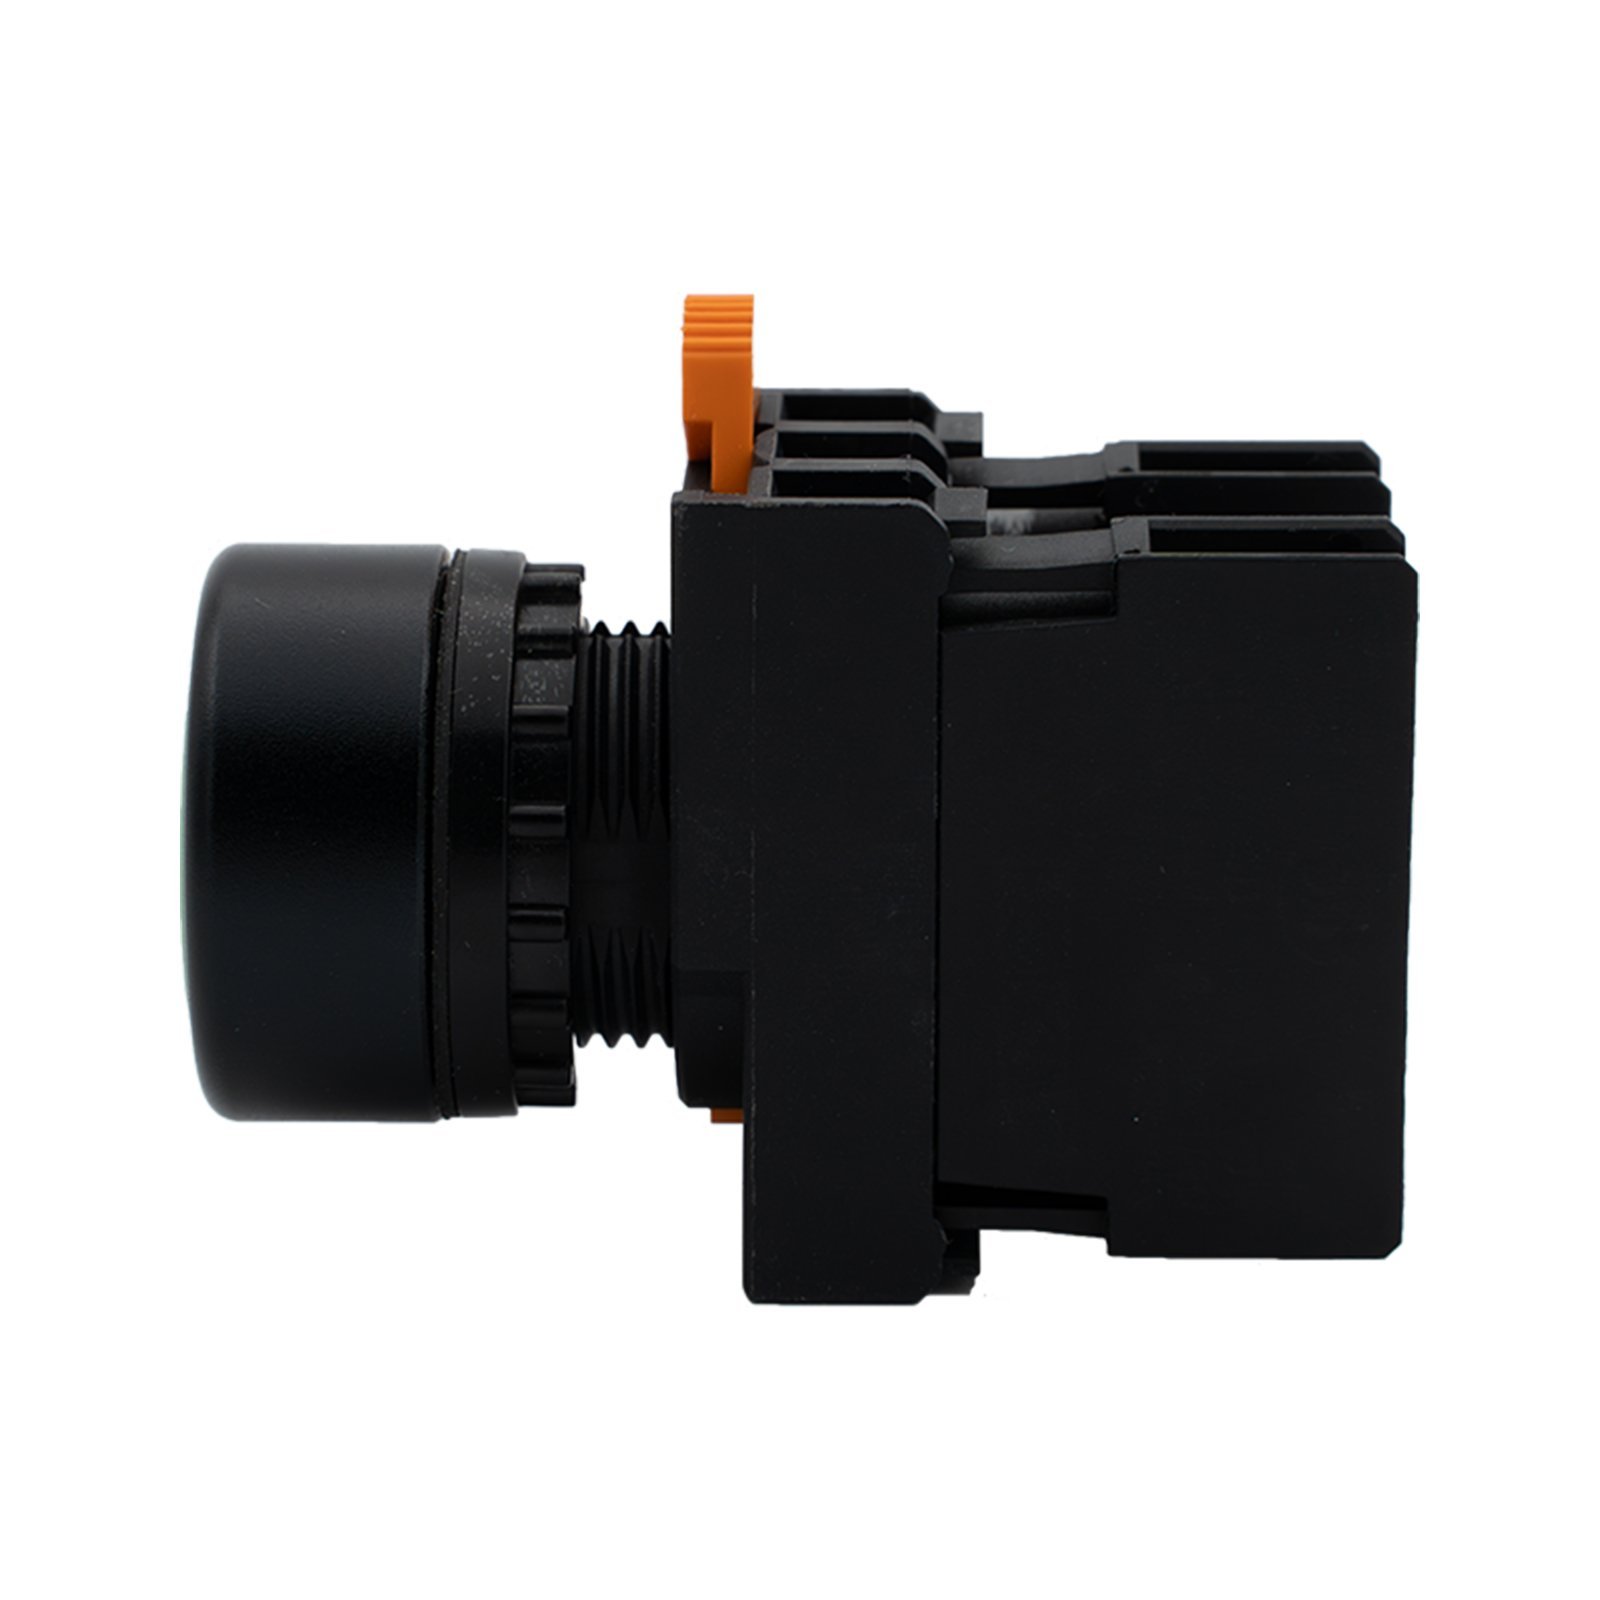
- Check the sealing ring. It should sit in its groove, unbroken, with no flat spots. A missing or pinched gasket will not pass water on the machine, and it is invisible once the button is in the door.
- Test thread the collar. Onto a spare frame, or a scrap of panel if that is what you have. A collar that fights a fingertip turn here will fight a torque wrench on install day, and it is cheaper to find out now.
- Photograph every fault, carton label in frame. A claim carrying a batch number and a photo settles in one message. A claim without them collects a week of emails.
What to have ready before the truck arrives
Most dock checks fail for want of preparation, not time. The kit is small. The purchase order. Printed, or on a phone. Memory of what you ordered drifts first, always. The model code table, on actual paper. A phone screen and a dusty carton are a bad combination, as anyone who has tried both knows. A multimeter that someone has trusted recently. A torque driver, if collar checks are in your routine. And a roll of tape. The fastest quarantine in existence is a taped lid with a word written on it in marker.
One habit beats every tool in that kit. Decide the sampling plan before the driver arrives, not while he waits. Three cartons from different layers of the pallet is a plan. Opening whatever is on top and stopping after the first good tray is a ritual, and rituals find nothing.
Illuminated units take one more minute each
Lighted buttons carry a second circuit, and that circuit wants its own minute. Read the voltage marking on the LED block and match it to the PO. A 110 V lamp block wired to a 24 V supply will not complain at the dock. It complains in the field, months later. Polarity marking on the terminal side: legible or not? That is the whole check. If you can wire a sample to a suitable supply, do it, then watch the lens for a few seconds instead of glancing. A dim or flickering fresh unit hides a solder or resistor fault, and continuity testing will never find it. On our own XH2 illuminated units the LED block is a separate low level circuit at 15 mA or less, so lamp faults never masquerade as contact faults, but only if the two were ordered correctly in the first place.
Reading what you find
Nearly every finding drops into one of three buckets, and the bucket tells you who does the fixing. Loose parts, shifted trays: transit. Note it, keep the packaging, and the claim is easy. Several units from one tray with a gritty return or a scorched face? That is workmanship. Sample wider from that tray and quarantine it. And then there is the wrong variant: a latching where you ordered momentary. A picking error, and the nastiest of the three, because you cannot see it on the part. You see it when the machine behaves differently, and it bites hardest in the bouton-poussoir momentané lines where the mix-up looks identical.
The awkward middle case is a single unit with a small defect in a large shipment. One stiff collar out of five hundred pieces is not worth a rejection. That outcome costs both sides money. Take the hold-note route instead. Accept the shipment, flag the serial range, and send the photos through the page de contact in one message. Every maker we know in this trade would rather replace three units than argue about them.
The paperwork half of the routine
Half the value of a dock check is on paper. Match the packing list to the PO, line by line. Totals can match while lines do not. Write down the batch or date code printed on the carton and keep it with the receiving record. Any field complaint later traces through that code faster than through any invoice. File one photo of the goods as they arrived, trays still intact, before anything moves. Three months later, when somebody asks what actually arrived, the photo answers in minutes.
Importers running their first shipment of a new variant should widen the sample. A first order of a latching variant, for instance, deserves a dozen units operated and ringed out, not three, because the mechanism is new to your line and your assemblers. By the second shipment the sample can shrink back.
What the routine catches that a certificate never will
Two examples from our own side of the dock, because they shape how we pack. A customer once received a batch where every tray of mushroom heads had shed its foam insert in transit, and the heads arrived polished but scratched. The parts were fine. The packing had failed. Since then, every mushroom variant ships with its inserts taped down. None of them ride loose any more. Another time a whole carton travelled with the collars backed off, and the receiving check found it in four minutes. The collars had been loosened at final inspection and never retorqued.
None of that shows on a test report. All of it shows in ten minutes at the tail lift, which is why we would rather our customers check than trust us.
The paperwork proves what the factory can do. The carton shows what actually left it. Ten minutes and a multimeter, sampled across the pallet, closes the gap between the two, and it is the cheapest quality control you will ever run.